 Kaizen is the Lean practice of continuous improvement through small changes, made constantly, by everyone. The word is Japanese: kai (change) and zen (good). In a kaizen workplace, improving the process is part of every job, from the operator who moves a tool rack closer to the press to the manager who removes an approval step. No single change is dramatic. The accumulation of thousands of them is what separates a Lean operation from one that only reorganizes when there is a crisis.
Where kaizen came from
The practice grew up inside the Toyota Production System after World War II, where Taiichi Ohno expected every worker to identify waste and fix it, and where the company's suggestion system eventually drew in hundreds of thousands of employee ideas a year. The word reached Western management through Masaaki Imai's Kaizen: The Key to Japan's Competitive Success (1986) and his follow-up Gemba Kaizen (1997), which argued that Japan's post-war industrial performance came less from technology than from a disciplined habit of continuous, incremental improvement. Imai founded the Kaizen Institute to teach the approach, and his framing is still the standard one.
Kaizen vs. innovation
Imai's central distinction was between kaizen and what he called innovation: the Western preference for large, infrequent, capital-intensive leaps.
| Kaizen | Innovation | |
|---|---|---|
| Pace | Small steps, continuously | Big steps, intermittently |
| Who | Everyone | A few specialists |
| Investment | Low cost, high effort to sustain | High cost, low effort to sustain |
| Risk of a bad change | Low; easy to reverse | High; hard to reverse |
| Results | Gradual, cumulative, durable | Immediate, then often erodes |
Neither is wrong. New equipment, new products, and new facilities are innovation and are sometimes the only way forward. Imai's point was that innovation without kaizen decays: the new line is installed, nobody improves it, and performance slides until the next capital project. Kaizen is what holds the gains and keeps improving them in between.
Principles of kaizen
Everyone participates
The people doing a job know its problems better than anyone observing it. Kaizen depends on them having the authority to make small changes to their own work and a simple way to propose larger ones. Where every change needs a manager's sign-off, improvement stops at the manager's capacity.
Respect for people
This is the condition that makes participation possible. Workers will not suggest improvements if suggestions are ignored, if problems are blamed on the person who found them, or if "improvement" only ever means cost cutting that lands on them. In practice: every suggestion gets a response, problems are treated as process failures, and improvements that make the work safer or easier count as much as ones that save money.
Go to the gemba
Gemba is the place where the work happens. Kaizen problems are observed on the floor, not inferred from reports in a conference room. The gemba walk, where managers go to the floor to see the process and ask questions, is the management habit that keeps kaizen honest.
Standardize, then improve
There is no improvement without a standard to improve against. Kaizen and standard work are a cycle: document the current best method, improve it, document the new method, repeat. An improvement that is not written into the standard is lost at the next shift change.
Decide with data
Before-and-after measurement is what turns an opinion into an improvement. It does not need to be elaborate. A tally sheet and a stopwatch cover most kaizen.
Management's role
Kaizen fails most often not on the floor but above it. Management's job is to:
- Set the direction, so improvement effort points at what matters to the business rather than scattering.
- Respond to every suggestion, quickly, even when the answer is no.
- Protect time for improvement. A team with no slack cannot improve anything.
- Maintain the standards and make sure changes to them are documented and communicated.
- Show the data behind management's own decisions, so people see that changes are purposeful.
- Practice kaizen on their own work, visibly.
Daily kaizen vs. kaizen events
Kaizen operates at two speeds, and a mature program runs both.
Daily kaizen
Small improvements made continuously as part of normal work: a suggestion board, a five-minute daily huddle where problems are raised, operators adjusting their own area. Individually tiny, collectively the main source of improvement in a Lean plant. Toyota's suggestion system is the model; Toyota's own description of how kaizen works in its plants is a useful reference.
Kaizen events
A kaizen event (also called a kaizen blitz or rapid improvement event) is a focused, scheduled project in which a cross-functional team improves one process over a short period, usually three to five days. Events are for problems too large for daily kaizen: a cell layout change, a changeover reduction, a 5S implementation in a new area, a workflow redesign. The format:
- Preparation (two to four weeks before). Pick the process, write a one-page charter with the problem, the target, the scope, and what is out of scope. Collect baseline data. Select a team of five to eight: people who do the work, a facilitator, and one or two from outside the area for fresh eyes. Notify affected departments.
- Day 1: observe. Train the team on the tools if needed, then go to the gemba. Map the current process, time it, and identify waste. Begin root cause analysis on the biggest problems.
- Days 2 and 3: change. Brainstorm, pick the countermeasures, and implement them on the floor during the event, not in a report afterward. Move the rack. Re-mark the floor. Try the new sequence and time it again.
- Day 4: standardize. Document the new standard work, update visual controls, train the shifts that were not in the room.
- Day 5: report and plan follow-up. Present results to leadership with before-and-after data. List the items that could not be finished in the week on a follow-up plan with owners and dates.
- 30-day follow-up. Audit whether the new standard held and the follow-up items got done. This is the step most often skipped and the reason most event gains fade.
The most common event failure is scope creep: a week scoped to one process expands to the whole department and nothing gets finished. The charter's out-of-scope line and a parking lot for good ideas that belong in a future event are the defense.
Tools of kaizen
PDCA
Plan-Do-Check-Act is the improvement cycle at the center of kaizen. Plan: define the problem, analyze the cause, and decide on a change and the result you expect. Do: make the change, on a small scale if possible, and collect data. Check: compare the result with what you expected. Act: if it worked, standardize it; if not, learn why and go back to Plan. Every kaizen event and most daily improvements are a PDCA loop.
5S
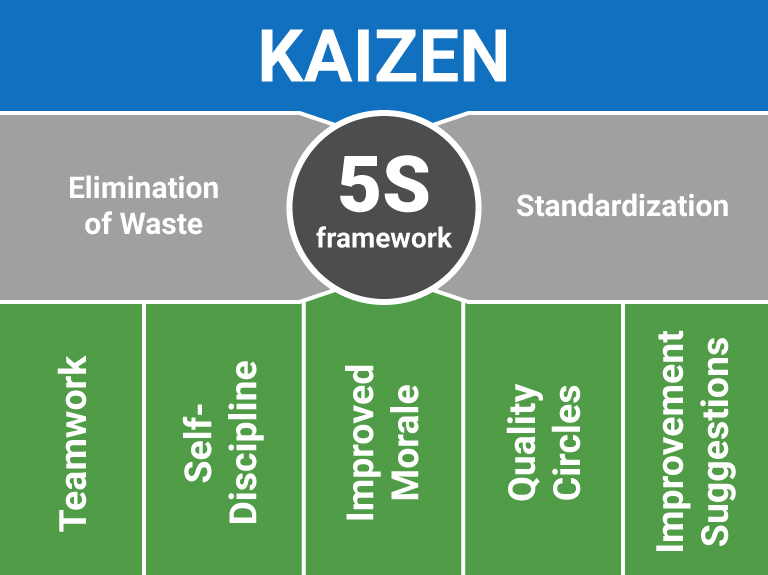 5S is usually the first kaizen a facility does and the foundation for the rest. A sorted, organized, standardized workspace makes waste visible, which is what gives daily kaizen something to work on, and it builds the habit of auditing against a standard. Most kaizen events in a new area start with 5S.
Quality circles
Small groups of workers from the same area who meet regularly to identify and solve problems in their own work, using simple tools. Quality circles came out of Japanese quality control in the 1960s and are the organized form of daily kaizen. TQM adopted them wholesale.
A3 and suggestion systems
An A3 is a one-page problem-solving report (named for the paper size) that walks through background, current condition, target, root cause, countermeasures, plan, and follow-up. It is the standard format for a kaizen project at Toyota and many Lean companies. A suggestion system is the lighter-weight version: a card or board where anyone can propose an improvement, with a visible process for responding.
Root cause analysis, Pareto, and the seven tools
Kaizen problem-solving uses the basic quality tools: the 5 Whys and fishbone diagrams for root cause analysis, Pareto charts for choosing what to work on first, check sheets and simple charts for measuring results.
Benefits
 The direct results are the ones Lean promises generally: shorter lead times, less inventory, fewer defects, lower cost, safer work areas. The distinctive result of kaizen is that these keep improving rather than being achieved once and defended. The cultural result is that problems get raised instead of hidden, because raising a problem is how improvement starts rather than how blame gets assigned.
Frequently asked questions
What does kaizen mean?
"Change for the better" or "good change." In Lean it means continuous improvement through small, frequent changes made by everyone in the organization.
What is a kaizen event?
A focused improvement project, usually three to five days, in which a cross-functional team analyzes one process, implements changes on the floor, and documents the new standard.
What is the difference between kaizen and continuous improvement?
Kaizen is the Japanese term and the specific Lean practice; continuous improvement is the general English concept. In most Lean contexts they are used interchangeably.
Is kaizen the same as 5S?
No. 5S is a specific method for organizing a workspace. Kaizen is the broader practice of continuous improvement, of which 5S is usually the first step.
How is kaizen different from Six Sigma?
Kaizen is small, frequent, floor-driven improvement with simple tools. Six Sigma is project-based, statistically driven, and led by trained practitioners. They are complementary; kaizen handles the many small problems and Six Sigma the few chronic, complex ones.
Related resources
For the broader system kaizen belongs to, see Lean manufacturing. For the tools, see 5S, root cause analysis, kanban, and TPM. The Lean Enterprise Institute's lexicon entry on kaizen is a concise authoritative definition. 5S Today stocks the Lean manufacturing tools and kaizen training videos used in events and daily kaizen.