Kanban is the Lean system for controlling production and inventory with signals. Instead of making or ordering parts according to a forecast, each step in a process produces or replenishes only when the next step signals that it has consumed something. The signal is the kanban: a card, an empty bin, a marked space on the floor, or an electronic message. Kanban is how a pull system is run in practice, and it is the mechanism that makes just-in-time production work.
The word is Japanese for "signboard" or "visual signal." Since the 2000s the term has also been used for a workflow management method built on boards and work-in-progress limits, mostly in software and office work. That method borrows the name and the pull idea from manufacturing kanban; it is covered in its own section below.
Where kanban came from
Taiichi Ohno developed kanban at Toyota in the late 1940s and 1950s as part of the Toyota Production System. His model was the American supermarket, where shelves hold a small stock of each item and are restocked only as customers take things, rather than by a schedule. Applied to a factory, the "customer" is the downstream process and the "shelf" is a small buffer of parts between steps. When the downstream process takes parts, it sends a signal upstream, and only then does the upstream process make more. Overproduction, which Ohno considered the worst of the seven wastes, becomes impossible: nothing is made without a signal, and the number of signals in circulation caps the inventory.
How a kanban system works
The simplest form is the two-bin system. A workstation keeps two bins of a part. The operator draws from the first. When it is empty, the empty bin (or the card attached to it) goes back to the supplying process or stockroom as the signal to refill, and the operator works from the second bin. The refilled first bin returns before the second runs out. The bin quantity is set so that one bin covers consumption during the replenishment lead time, with a safety margin.
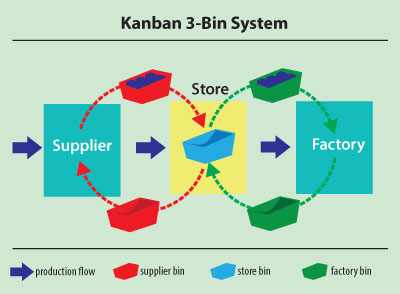
The three-bin system extends this across a supplier boundary: one bin at the point of use, one in the plant's store, and one at the supplier. When the point-of-use bin empties, it is swapped with the store bin; the store's empty bin signals the supplier to ship the third and begin filling a replacement. Each bin is a kanban, and the three together hold exactly the inventory needed to cover the full replenishment loop.
In a card-based system the same loop runs with two kinds of card:
- Withdrawal kanban (also called move or conveyance kanban) authorizes moving a standard quantity of a part from the upstream store to the downstream process. It travels with the parts and returns to the store when the container is emptied.
- Production kanban authorizes the upstream process to make a standard quantity to replace what was withdrawn. When a container leaves the store, its production kanban goes to the upstream process's scheduling board, and that process makes exactly that quantity, in the order the cards arrived.
A kanban card carries the part number and name, the container type and quantity, the supplying process and location, the consuming process and location, and often a barcode. Three less common types handle exceptions: express kanban for a shortage, emergency kanban to replace defective parts, and through kanban, which combines withdrawal and production cards when two processes are adjacent.
Ohno's rules for kanban
Ohno set six rules that keep a kanban system from decaying into an ordinary inventory system.
- The downstream process withdraws only what it needs, when it needs it, in the quantity on the kanban.
- The upstream process produces only what was withdrawn, in the quantity and sequence of the kanbans received.
- Nothing is produced or moved without a kanban.
- A kanban is always attached to the parts it authorizes.
- Defective parts are never sent downstream. A defect stops the loop until it is fixed.
- The number of kanbans is reduced over time. Fewer cards means less inventory, which exposes the problems the inventory was hiding, which are then fixed. This is how kanban drives kaizen.
How many kanbans do you need?
The standard formula sets the number of cards (or bins) in circulation for a part:
Number of kanbans = (Average daily demand × Replenishment lead time in days × (1 + Safety factor)) ÷ Container quantity
For a part consumed at 200 per day, replenished in 2 days, with a 20% safety factor and 100 per container: 200 × 2 × 1.2 ÷ 100 = 4.8, rounded up to 5 kanbans. That caps inventory of the part at 500 pieces. The safety factor covers variation in demand and lead time; as the process stabilizes it is reduced, following Ohno's sixth rule, and the number of kanbans with it.
Electronic kanban
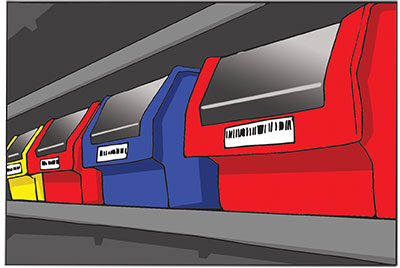
Many facilities now run the signal electronically: a barcode scan on an empty bin, a button at the workstation, or a trigger from the ERP system generates the replenishment order. E-kanban removes lost cards, gives a real-time view of the loop, and works across sites and suppliers. Most plants still keep the physical bin and label at the point of use, because the empty bin on a marked shelf is a signal anyone can see without a screen, and the physical limit on bins is what stops inventory from creeping up.
Kanban and the visual workplace
Kanban only works if the signal is unmistakable, which makes it a 5S problem as much as a scheduling one. Each part needs a marked home, usually a floor-marked square or a labeled shelf position sized for exactly the number of containers in the loop. An empty square is the signal. Cards and bins need durable labels with the part number, quantity, and locations, printed on stock that survives the shop floor. A kanban post or board at each supplying process holds the production cards in the order they arrived. If any of these are missing, operators start guessing, and guessing is the forecast the system was built to replace.
Benefits
- Overproduction stops. Nothing is made without a signal.
- Inventory is capped and visible. The number of kanbans is the maximum stock, and anyone can count the bins on the shelf.
- Problems surface. A late supplier, an unreliable machine, or a quality problem stops the loop immediately instead of being absorbed by a pile of safety stock. That is uncomfortable by design.
- Scheduling simplifies. Upstream processes build what the cards say, in card order. No central schedule, no expediting list.
- Operators control replenishment. The person who empties the bin triggers the refill. No requisition, no planner, no waiting.
- Demand changes propagate automatically. If consumption rises, cards cycle faster; if it falls, they sit. Adjusting the number of cards adjusts capacity.
Kanban boards and the Kanban Method
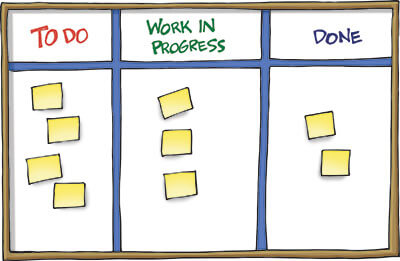
In the mid-2000s David Anderson adapted manufacturing kanban into a method for managing knowledge work, first at Microsoft. The Kanban Method keeps the pull principle and the visual signal but applies them to tasks rather than parts. Its core practices:
- Visualize the workflow on a board with a column for each stage (to do, in progress, review, done) and a card for each work item.
- Limit work in progress by capping the number of cards allowed in each column. A full column means nothing new can enter until something leaves, which is the pull signal.
- Manage flow by measuring how long items take to cross the board and removing what slows them.
- Make policies explicit: what "done" means for each column, how work is prioritized.
- Improve collaboratively using data from the board.
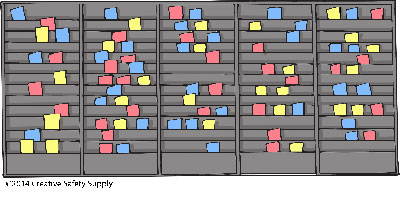
Boards can be physical (a wall, sticky notes, visible to everyone in the room, no software) or electronic (shared across sites, searchable, with automatic metrics). The choice is about where the team sits. For how the method compares with other iterative approaches, see Agile vs. Scrum. Manufacturing teams also use kanban boards for maintenance backlogs, engineering changes, and kaizen follow-up lists, where the work is tasks rather than parts.
Common misconceptions
"Kanban is just a card." The card is the signal. The system is the rules about what the signal authorizes, the number of signals in circulation, and what happens when the loop stops.
"Kanban means zero inventory." Kanban sets inventory at the minimum needed to cover replenishment lead time, then reduces it as the process improves. It is a controlled buffer, not no buffer.
"Kanban replaces planning." It replaces detailed production scheduling for repetitive parts. Capacity, staffing, and the number of kanbans still have to be planned, and demand that is highly variable or made-to-order usually needs a different approach.
"A kanban board is kanban." The board method is a legitimate descendant, but on a plant floor "kanban" means the pull signal for parts. The two share a name and a principle, not a toolkit.
Frequently asked questions
What does kanban mean?
Japanese for "signboard" or "visual signal." In Lean, the signal that authorizes a process to produce or move a specific quantity of parts.
What is the difference between push and pull?
Push production makes parts according to a schedule or forecast and sends them downstream whether or not they are needed. Pull production makes parts only when a downstream process signals that it has consumed some. Kanban is the signal.
What is a two-bin system?
The simplest kanban: two bins of a part at the point of use. When one empties it is returned for refilling and work continues from the second. The empty bin is the kanban.
How do I calculate the number of kanbans?
Daily demand, times replenishment lead time in days, times one plus a safety factor, divided by container quantity, rounded up.
Is kanban part of 5S?
No, but it depends on it. Kanban needs marked locations, labeled containers, and visual standards, which is what 5S provides.
Is kanban the same as Scrum?
No. Both are used in software, but Scrum works in fixed sprints with defined roles; the Kanban Method is continuous flow with WIP limits and no prescribed roles. See Agile vs. Scrum.
Related resources
Kanban is one of the core tools of Lean manufacturing and the mechanism behind the fourth Lean principle, pull. It works alongside kaizen, 5S, and TPM, and across supplier boundaries it is part of supply chain management. The Lean Enterprise Institute's lexicon entry on kanban is a concise authoritative reference. 5S Today stocks the labels, floor marking, and Lean manufacturing tools a kanban system runs on.